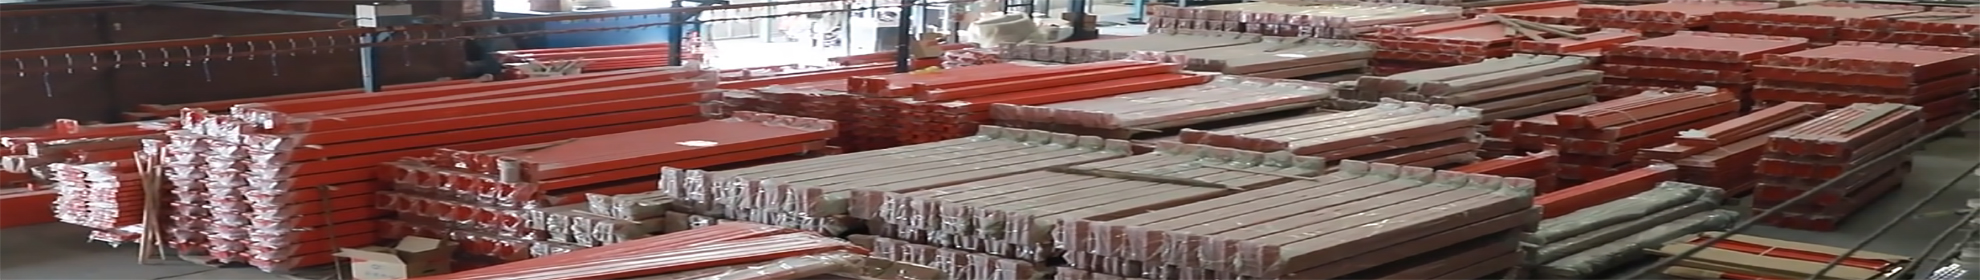
Project Overview:
In recent months, a leading logistics distribution center faced a critical challenge: a rapid increase in SKU counts and inventory volume was outpacing their available floor space. The existing storage method relied heavily on floor stacking, which resulted in low vertical space utilization, poor stock accessibility, and an increased risk of product damage.
To address these inefficiencies, our specialized engineering team was commissioned to design and install a high-density, heavy-duty storage system tailored to their fast-paced operations.
The Challenge:
Wasted Vertical Space:
The warehouse had 8 meters of clear height, but only the bottom 2 meters were being utilized.
Accessibility Issues:
"First-in, Last-out" (FILO) stacking made it difficult to access specific pallets, slowing down order fulfillment.
Safety Concerns:
Unstable floor stacks posed a potential risk to personnel and equipment.
The Solution: Heavy-Duty Selective Pallet Racking:
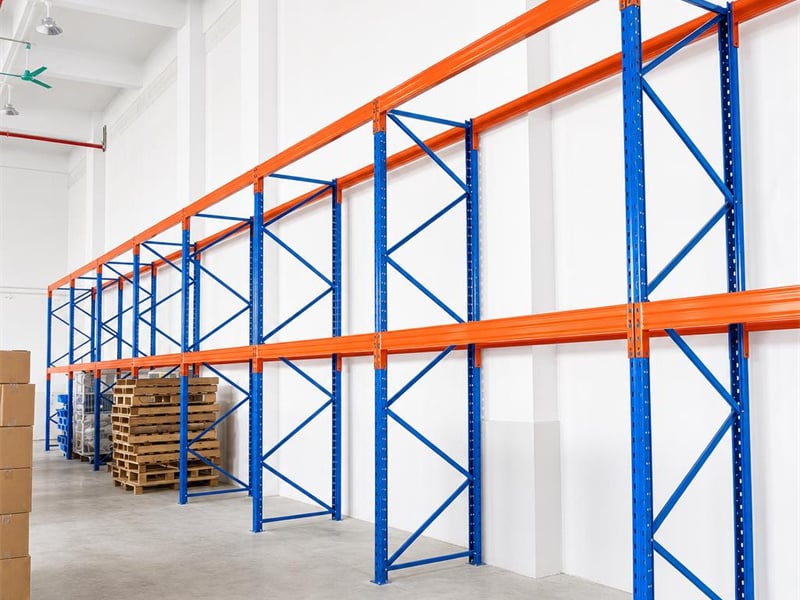
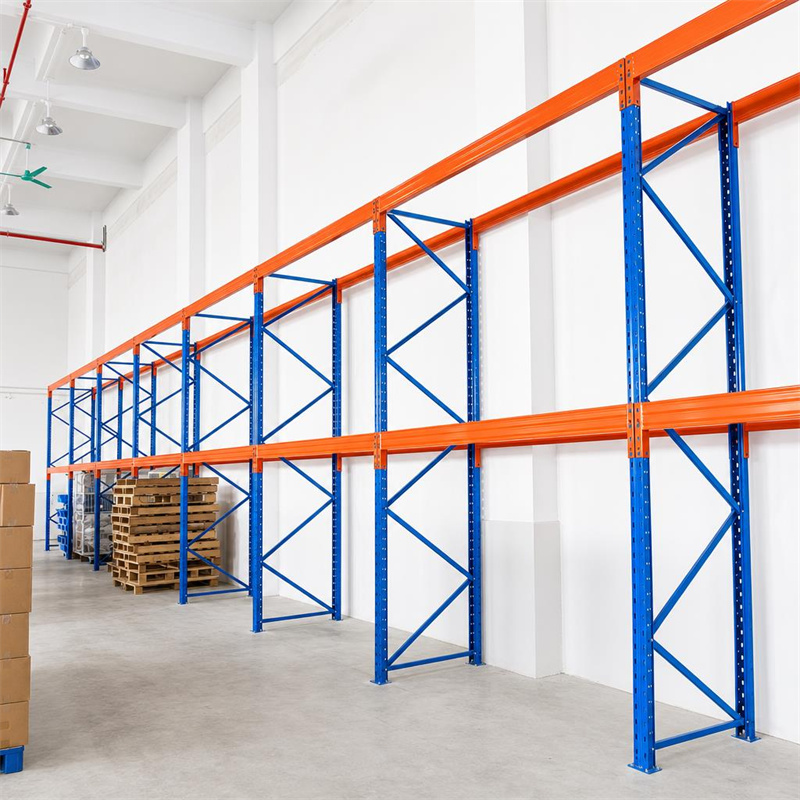
After a detailed site audit and load requirement analysis, we implemented a customized Selective Pallet Racking System. This solution was engineered to provide 100% accessibility to every pallet while safely utilizing the full height of the facility.
Key Technical Specifications:
Material: High-grade Q235 Cold-rolled Steel for maximum structural integrity.
Upright Design: Features precision-engineered Diamond-shaped holes (providing superior stability and easier beam adjustment compared to traditional teardrop designs).
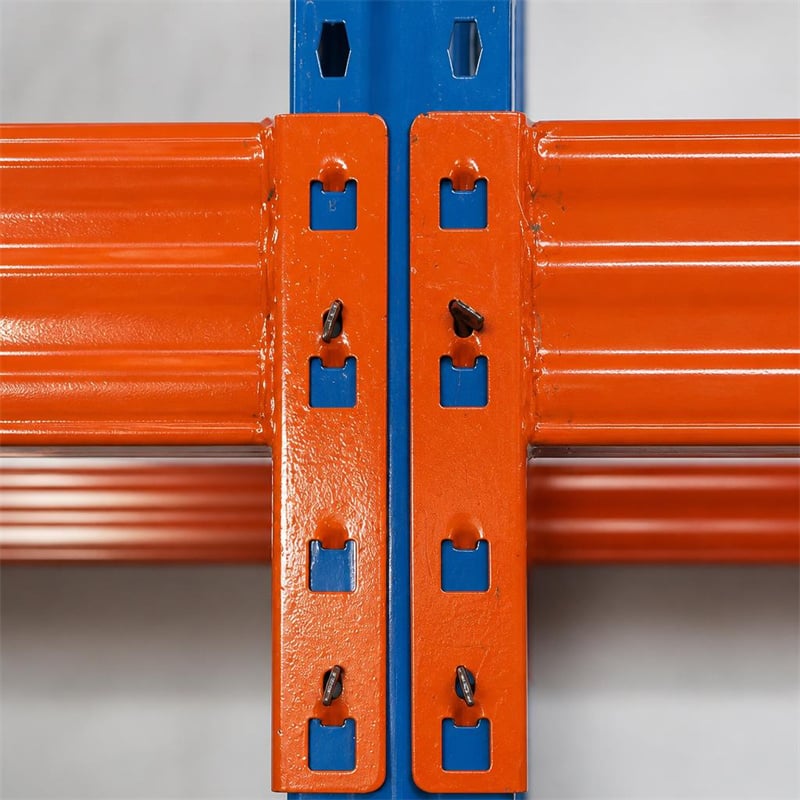
Finish: Automatic Electrostatic Powder Coating in professional Industrial Blue (Uprights) and Safety Orange (Beams) for long-lasting corrosion resistance and high visibility.
Load Capacity: Rated for 2,000kg per level, ensuring safety for heavy industrial components.
Compliance: Fully compliant with ISO 9001:2015, CE, and SGS standards.
Project Execution & Advantages:
The installation was completed in phases to minimize disruption to the client's daily operations. By shifting from floor stacking to a multi-tier racking structure, the warehouse achieved the following:
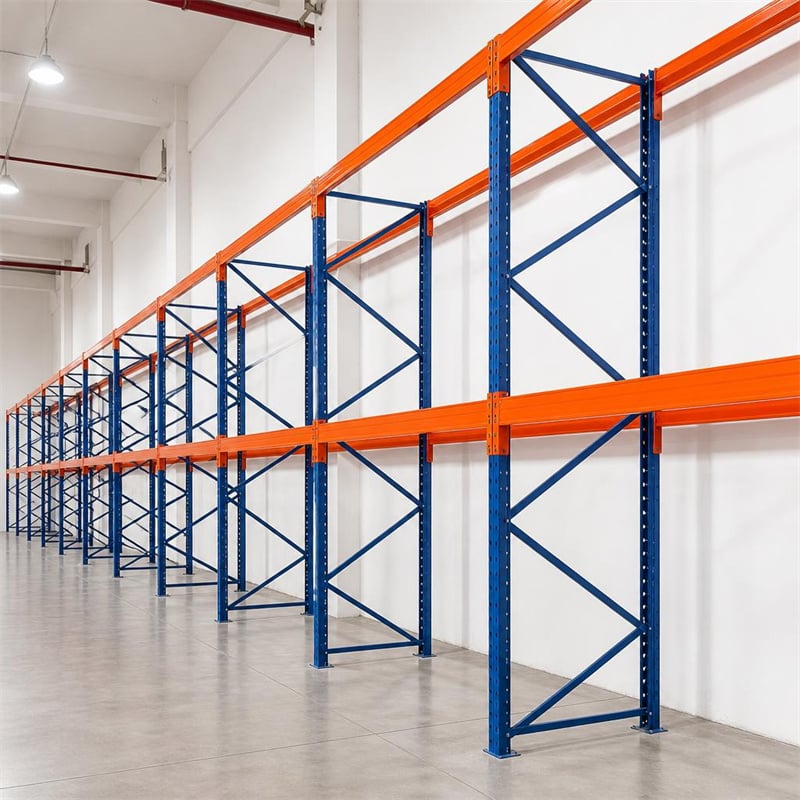
1.60% Increase in Storage Capacity: By utilizing the vertical cube, the client was able to store 3 times the amount of inventory within the same footprint.
2.Optimized Workflow: 100% pallet selectivity allowed forklifts to retrieve any item instantly, reducing picking times by 60%
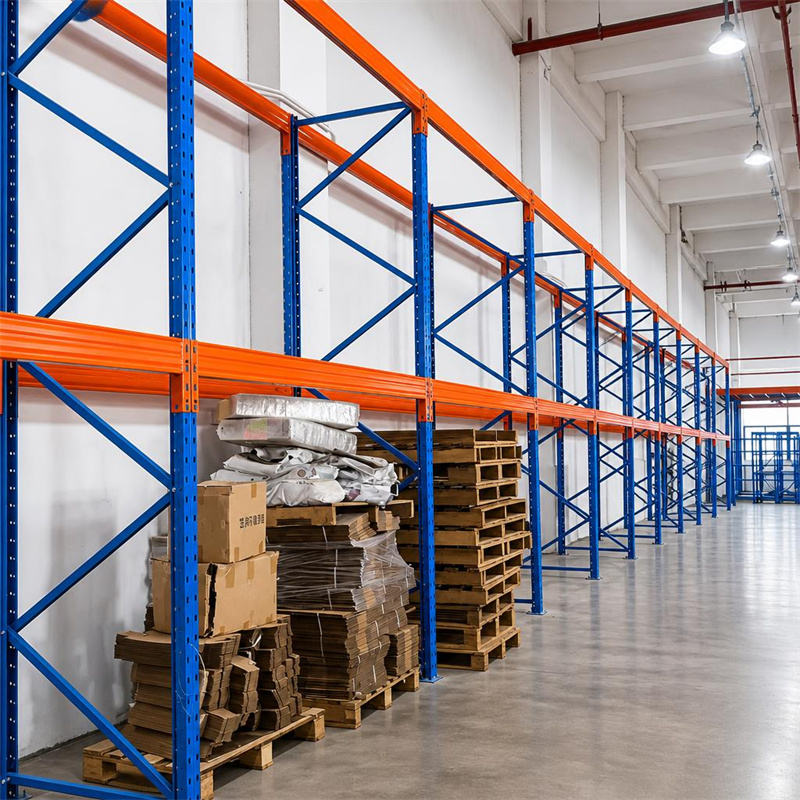
3.Enhanced Durability: The use of Q235 steel and electrostatic coating ensures the system remains maintenance-free even under heavy daily use.
4.Improved Safety & ROI: Organized storage reduced product damage by 30-40%, significantly improving the overall Return on Investment (ROI) for the facility.
This project demonstrates how a well-planned racking layout can transform a congested warehouse into a high-efficiency distribution hub. Our focus on using premium materials like Q235 steel and specialized designs such as diamond-shaped holes ensures that our clients receive a storage solution that is as durable as it is efficient.
For warehouse operators looking to optimize their storage density and operational speed, customized heavy-duty racking remains the most cost-effective and reliable strategy available today.

Transform your warehousing logistics operations with Maobang's unbeatable custom storage solutions at factory direct prices. Our expert team will work closely with you every step of the way to ensure your storage space is tailored to your exact needs.
Copyright © Guangzhou Maobang Storage Equipment Co., Ltd. All Rights Reserved - Privacy Policy
 EN
 AR
 FR
 DE
 EL
 IT
 JA
 KO
 PT
 RU
 ES
 SV
 TL
 ID
 VI
 TH
 MS
 HMN
 KM
 LO
 MR
 TA
 MY
 SD

